Drawing Review and Inspection Follow-up
We worked with a customer on a custom cooling roll that needed to fit an existing machine. The project required close attention to the roll dimensions, shaft-end connections, internal cooling arrangement and surface requirements. We followed the work through drawing revisions, inspection, roll-body rework and a further inspection.
Confirming the Installation Dimensions
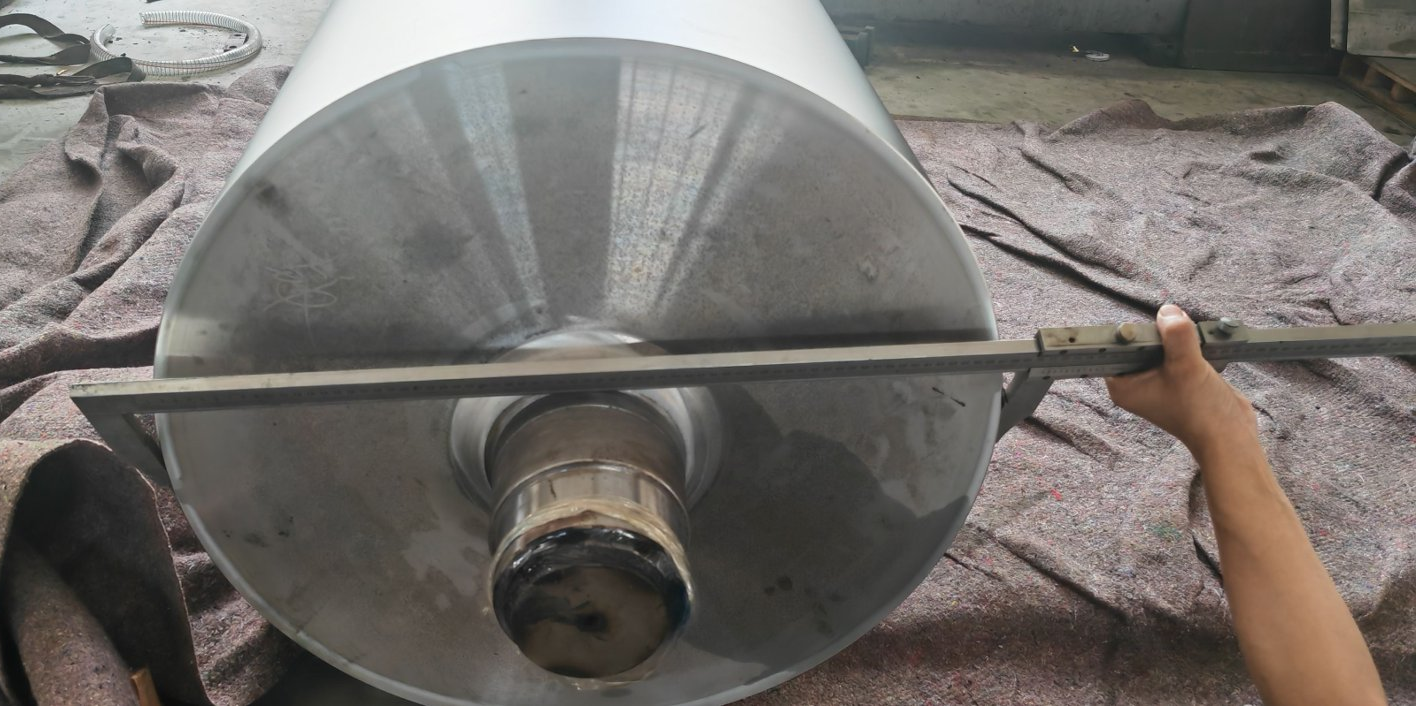
The customer's machine had limited adjustment available, making the roll diameter an important installation constraint. We reviewed the outside diameter, working-face length, shaft-end dimensions and keyway details with the customer.
During the project, a smaller outside diameter was proposed as an alternative. We checked this option with the customer, but it did not suit the available machine adjustment. The required diameter therefore remained a key condition in the subsequent roll-body work.
Reviewing the Drawings and Technical Requirements
The drawing discussions included changes to the shaft-fit requirement and additional information about the keyway. We followed these revisions alongside the other installation dimensions.
We also reviewed the internal cooling arrangement, rotary joints and chrome-plating requirements. These discussions covered the roll's internal structure as well as its external connections and working surface.
Following Surface and Dimensional Inspections
We arranged inspection visits and reviewed photographs, measurement records and progress updates. The inspections covered surface condition, roughness and dimensional checks.
The inspection findings identified points requiring further work on the roll surface. We tracked the additional surface treatment and arranged further checks of the surface condition and dimensions.
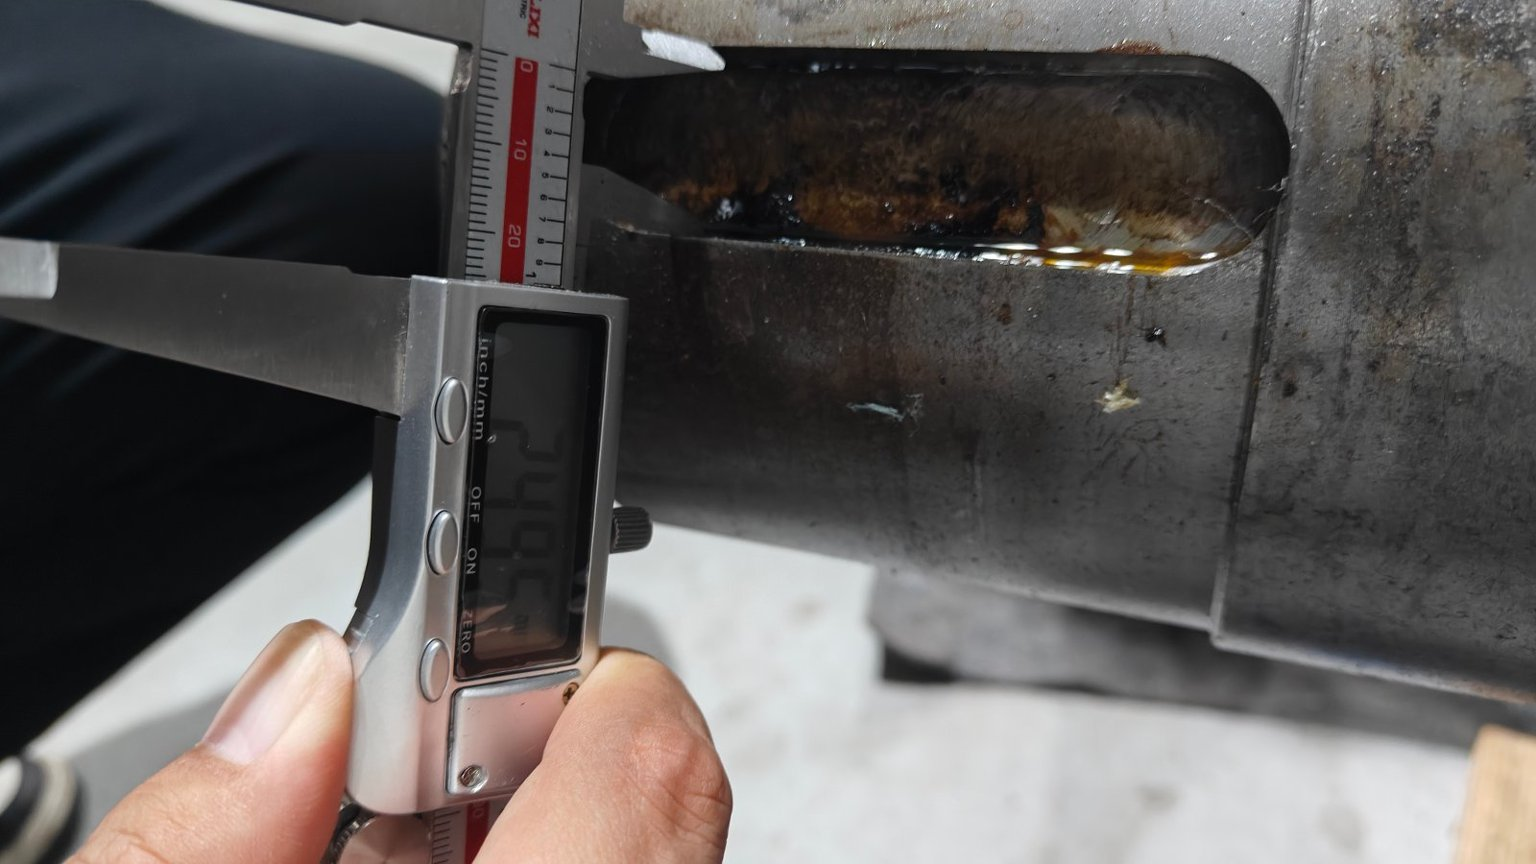
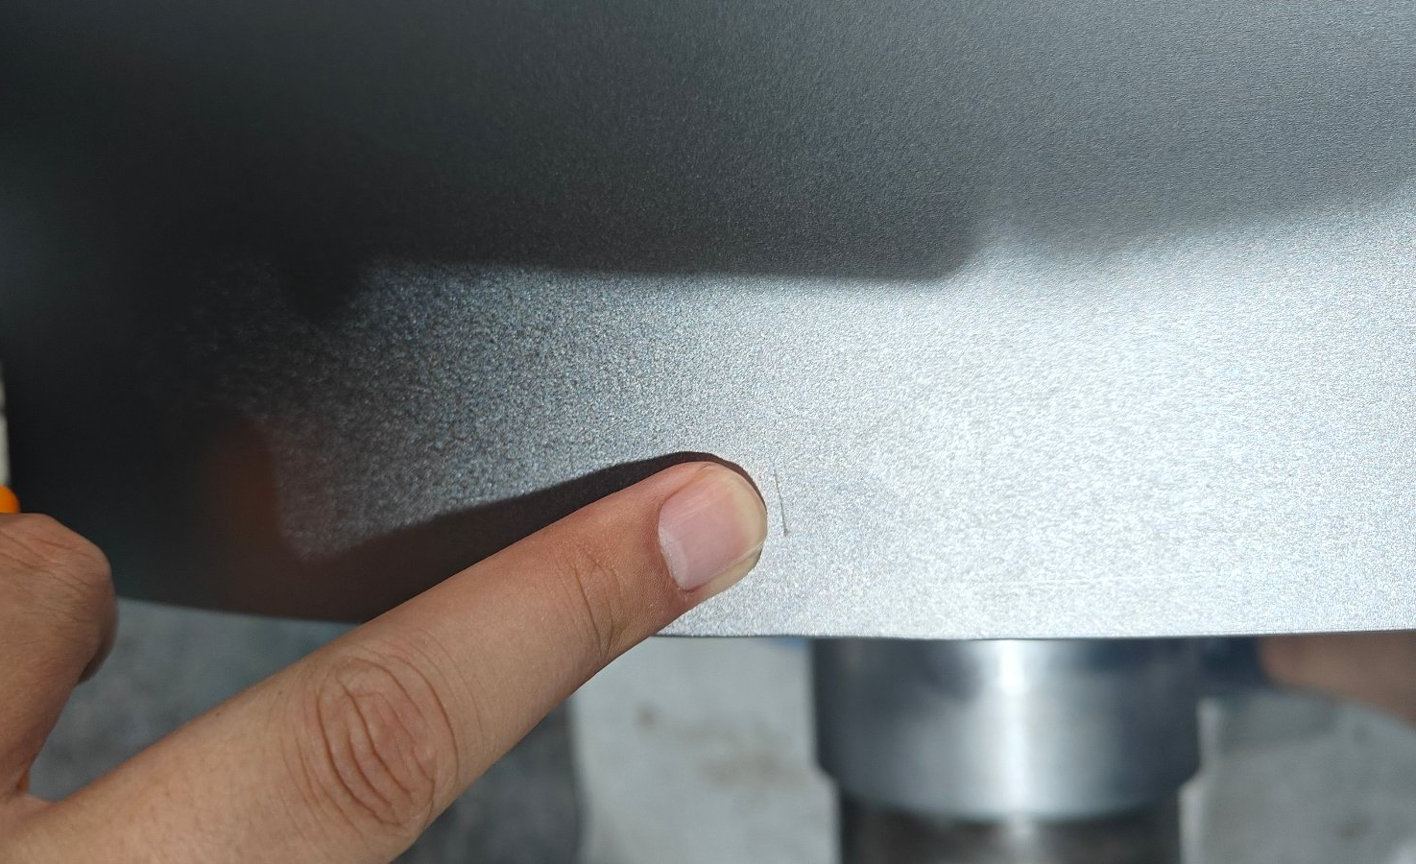
Earlier Inspection Stage
These photographs show a keyway dimension check and a visual review of the roll surface during the earlier inspection stage, before the subsequent roll-body rework.
Following the Roll Body Rework
The project later moved to a new roll body while retaining the shaft ends and inner assembly from the earlier assembly. We followed the dismantling, machining and reassembly stages through progress updates.
The shaft ends were removed, and the shaft ends and inner assembly were subsequently welded to the new roll body. We then tracked the surface-preparation work and arranged another inspection.
The roll-body work remained subject to the installation requirements discussed with the customer, particularly the outside diameter and shaft-end connections.
Following Up on the Updated Inspection Information
After the roll-body work, we followed up on another inspection and the associated photographs and inspection report for customer review.
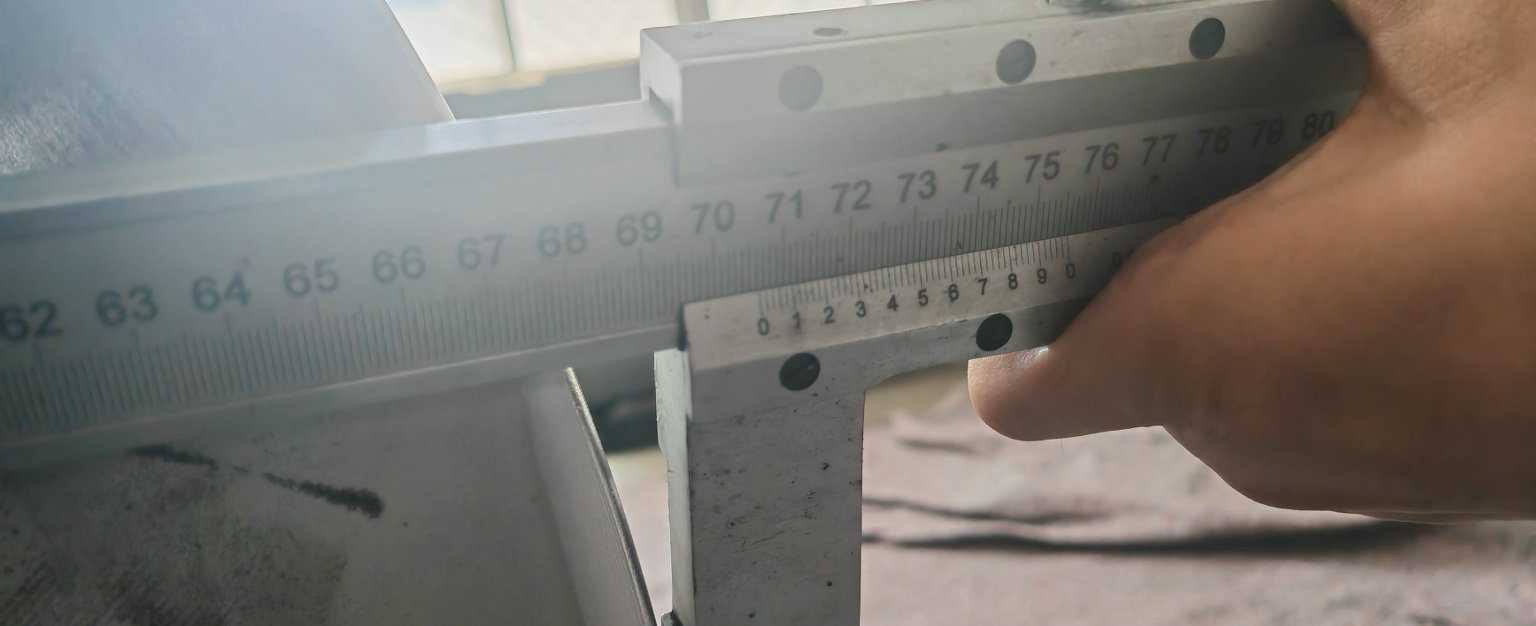
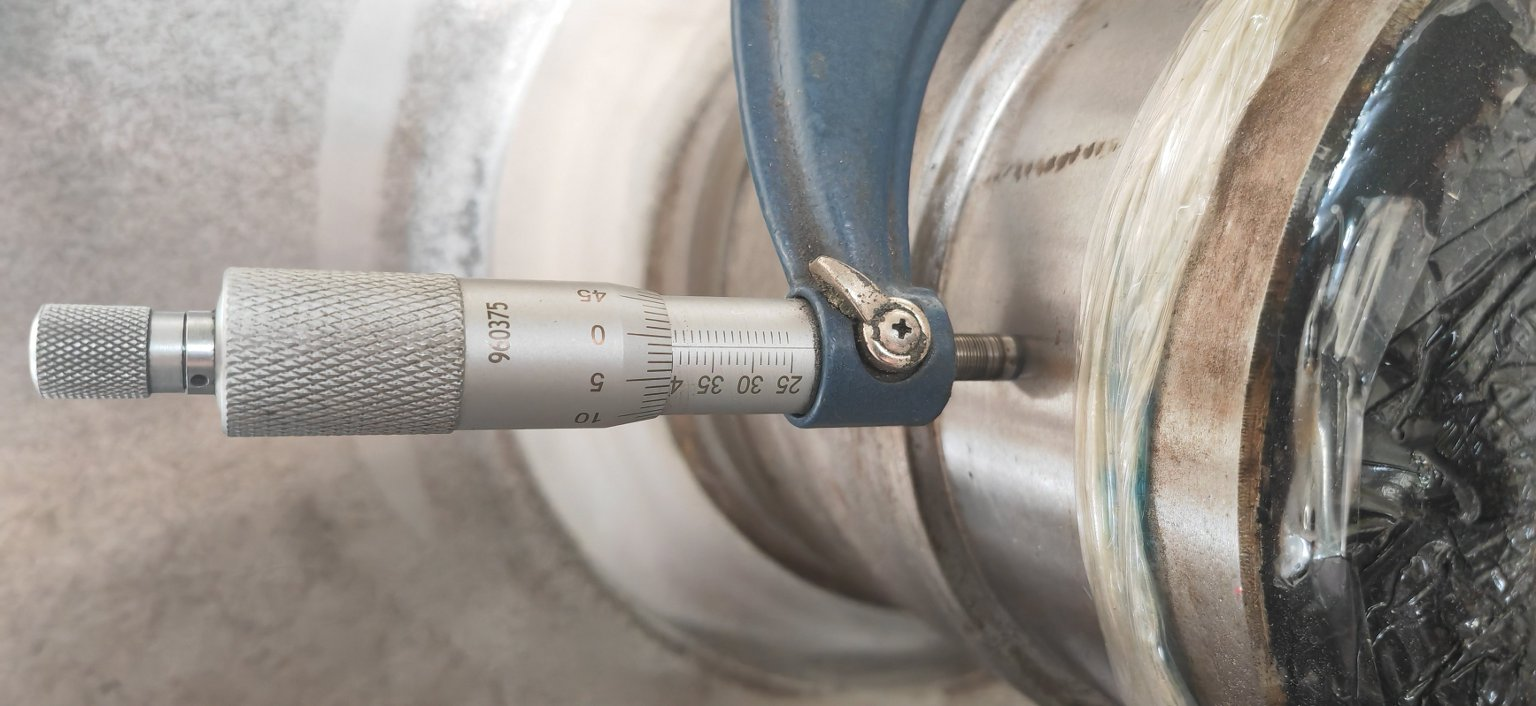
The photographs below show the roll-body outside-diameter check and a separate shaft-end diameter check from this follow-up inspection.
Our work throughout this cooling roll project focused on clarifying the technical requirements, following the processing stages and keeping inspection findings part of the subsequent discussions and work.
Cooling Roll Enquiry
Send us your roll drawing and installation dimensions, including the required shaft fits, keyways, cooling connections and surface specifications.
We can review the requirements with you and clarify the scope for quotation and inspection. Contact BANNOR or leave your question below.